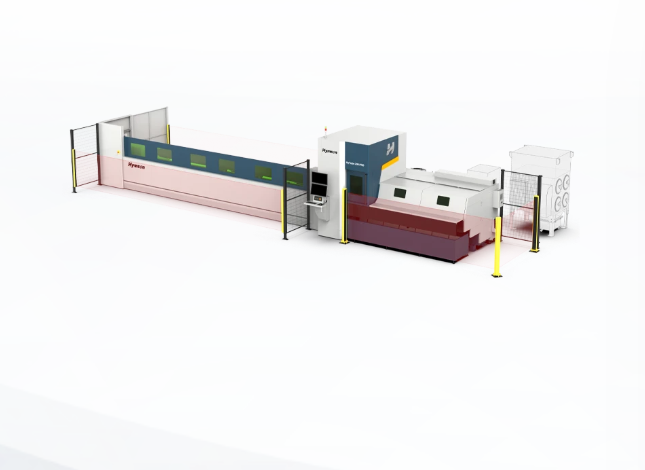
Key Questions Teams Must Resolve Before Choosing a Fiber Laser Pipe Cutter
Start with the problem you need the machine to solve
Teams often treat a fiber laser pipe cutter as a single solution, then discover it does not address specific production constraints. Define the core problem clearly: are you replacing a bottleneck, expanding part complexity, or seeking better edge quality? Evaluate a tube laser cutting system only after you map expected part families, takt time, and variability in raw material dimensions.
Material range and part geometry
List every material grade and wall thickness you will cut, including occasional outliers. Confirm whether the machine supports diameters, oval sections, and combined shapes you need. Complex bevels, piercing near joints, and thin-wall distortion require specific head types and control strategies. If a solution cannot demonstrate repeatable results for your hardest part, it will fail to meet expectations.
Throughput and cycle-time realism
Do not accept vendor cycle-time estimates without test data on your parts. Throughput depends on loading/unloading, fixturing, and post-process handling as much as laser power. Model complete cycle time for a realistic production shift and factor in changeovers for mixed batches. Short trials on representative lots expose hidden delays.
Integration with upstream and downstream processes
Machines do not live alone. Consider how the cutter will link to material storage, tube saws, benders, weld cells, and inspection stations. Confirm communication protocols, part marking, and nest planning with existing MES or CNC suites. Physical layout matters: access for forklifts, clearances for maintenance, and cable routing determine operational uptime.
Skills, training, and operator support
Procurement by cost alone ignores human factors. Identify the operator and maintenance skill set available today and the training plan to close gaps. Determine whether your team can program complex nests and troubleshoot beam-path issues, or if you require supplier-led service agreements. Operator competence influences scrap rates and tool life directly.
Maintenance, consumables, and spare parts strategy
Document mean time between failures for critical components and plan spare-part inventory accordingly. Laser sources, cutting heads, and chiller units have distinct service rhythms. Ask suppliers for local spares lists, expected life cycles, and repair turnaround times — long lead times for a consumable can stop production within hours.
Safety and regulatory factors
Laser installations demand zoning for access control, exhaust handling, and electrical compliance. Verify required permits and safety interlocks for your jurisdiction. Ignore these requirements and you risk forced downtime or fines.
Cost structure and return on investment
Compare total cost of ownership, not sticker price. Include installation, tooling, training, consumables, service contracts, and the cost of scrap during ramp-up. Set a realistic payback horizon tied to measurable KPIs: throughput per shift, reduction in secondary operations, or percentage of rework avoided.
Vendor capability, references, and proof
Demand reference visits, demonstration cuts on your parts, and clear performance guarantees. Review service coverage maps and escalation paths. Contracts should state acceptance criteria and penalties for missed service levels. Do not accept vague uptime promises.
Evidence, authority, and a real-world anchor
Practical procurement decisions rest on experience and measurable demonstrations. As a consultant who has advised fabrication shops through multiple equipment selections, I have observed what works and what does not. Major industry gatherings such as Fabtech in Chicago consistently reveal the same lesson: validated demos beat glossy brochures. Manufacturers present comparative benchmarks that you can verify in published proceedings, and attendees share field data openly. For a direct technical reference during evaluation, include a live cut on a cnc tube laser cutter using your hardest part; that single test prevents most post-installation regrets.
Common mistakes teams make
Teams cut to price, skip part-specific trials, assume vendor service is local, and underestimate training time. Avoid buying the highest-spec model without proving its value on your parts. Also avoid minimal documentation; demand baseline operating procedures and acceptance test reports before signing.
Decision checklist
Create a concise checklist: define problem statement, validate material and geometry, confirm true cycle time, verify integration points, map skills and training, secure spares and service, ensure regulatory compliance, obtain references and live demos, and compute full TCO. Use the checklist as a binding part of procurement scoring.
Synthesis and practical next step
Teams that align technical requirements, realistic throughput expectations, and service commitments reduce risk and shorten ramp-up. When specification sheets, demo cuts, and maintenance plans match your checklist, you have a defensible choice. For specification comparisons and documented service models, manufacturers commonly list field data and support structures through suppliers such as Hymson, which helps teams translate selection criteria into operational performance.